Reciprocating Grate Boilers
Continuous, Reliable Fuel Movement for Efficient Combustion
Reciprocating grate boilers provide a high-efficiency, low-maintenance, fuel-flexible solution for critical agro, industrial, and waste applications.
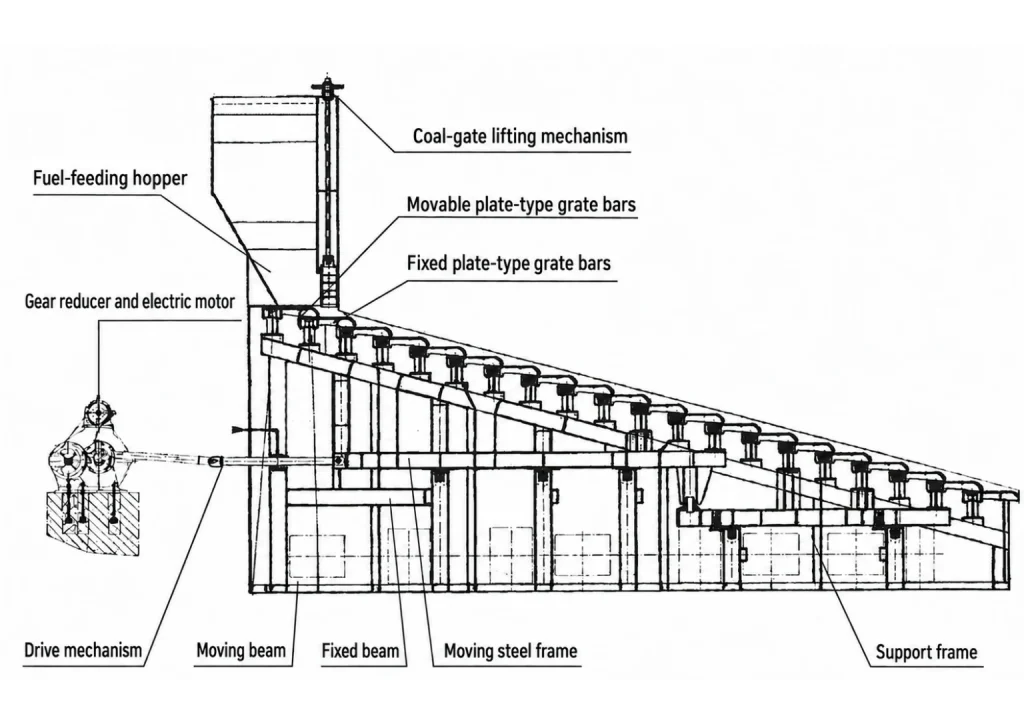
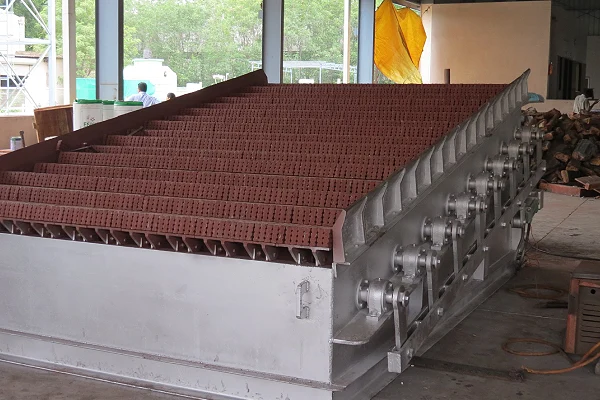
Reciprocating grate boilers are the best option for combustion of fuels with high moisture content, low calorific value, and variable particle size and shape. The reciprocating (pusher) grate combustion technology ensures complete combustion through continuous fuel agitation, resulting in high efficiency. The tumbling action enhances mixing, improves burnout, and accommodates variable fuel sizes and moisture content. These boilers are well suited for high-moisture agricultural waste and other industrial process waste.
Technical Specifications
Capacity
175 TPH
Pressure
125 Kg/cm²
Temperature
540°C
Design Variants
Single Drum
Bi Drum
USPs of Reciprocating Grate Boilers
- Tailored grate cooling – Versatile grate cooling design options available, matched to specific fuel characteristics
- Precision airflow control –Machined grate bars ensure proper clearances for thermal expansion, movement, and efficient airflow
- Sectional air control– Air plenum divided into multiple sections along the grate length, enabling independent airflow control per combustion requirement
- Adjustable combustion rate – Variable grate speed control
- Bulky fuel handling – Proven ram feeder design for handling bulky fuels
- Corrosion & wear resistance – Special alloy castings extend wear life and resist corrosion
Fuel Compatibility

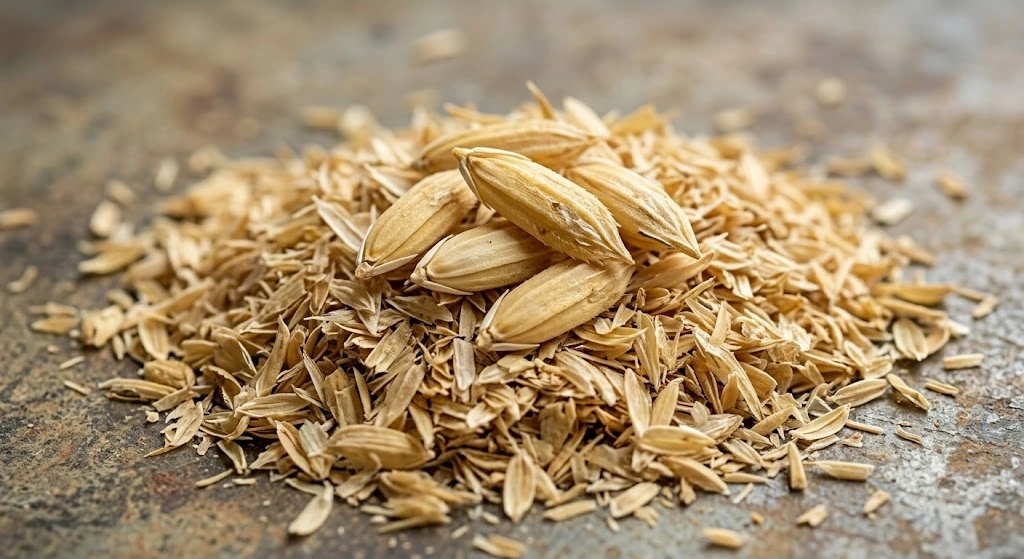
Rice Husk

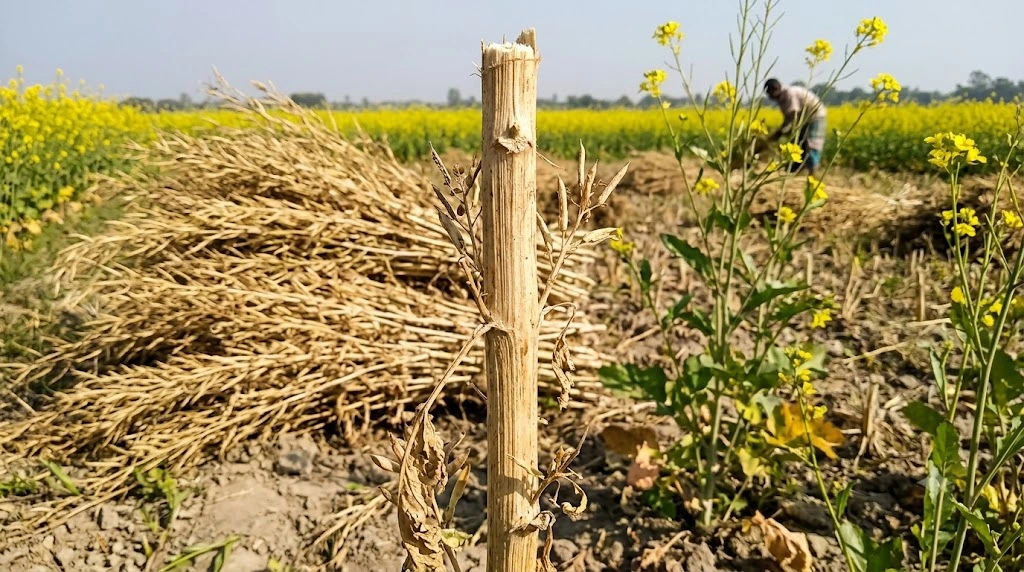
Mustard Stalk

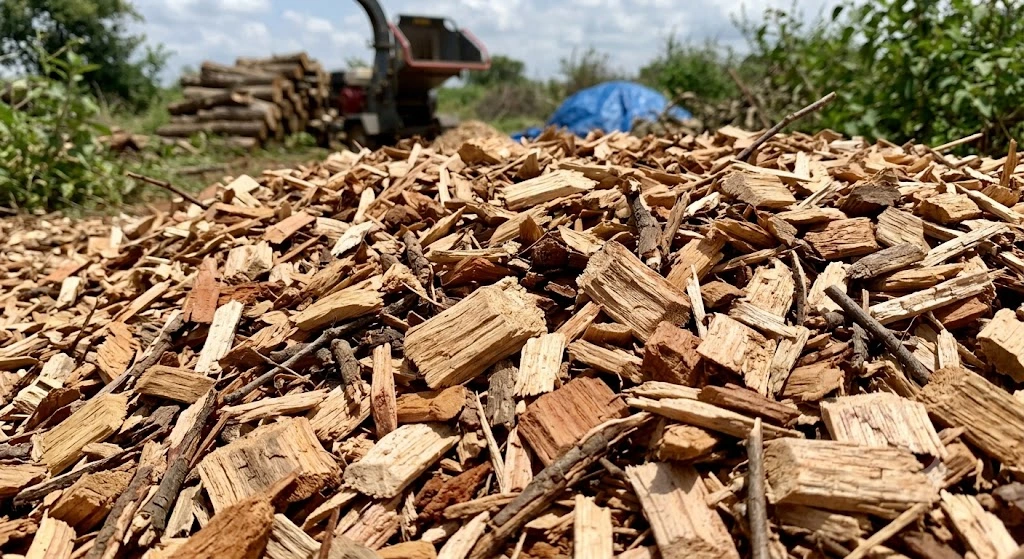
Wood Chips

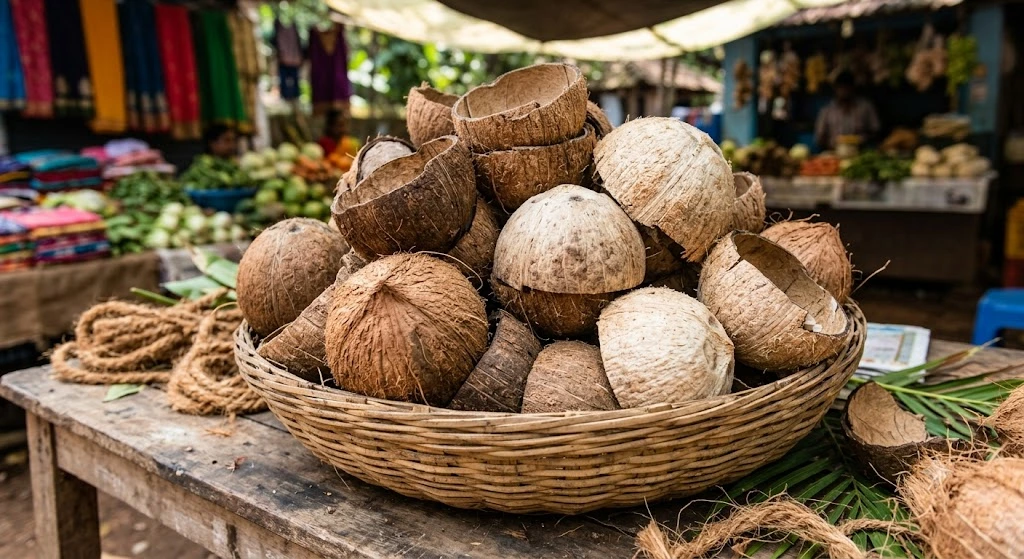
Coconut Shells

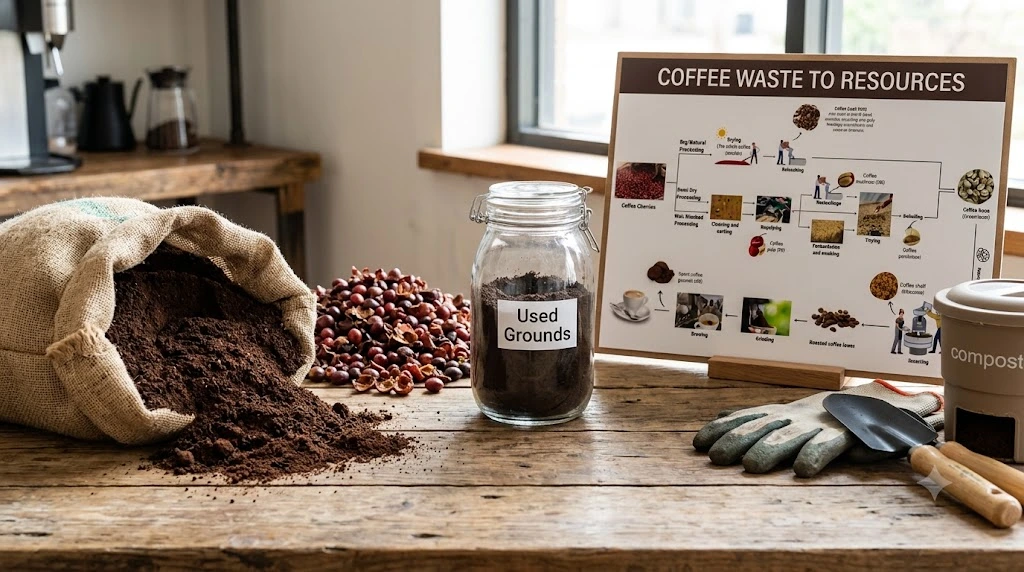
Coffee Waste

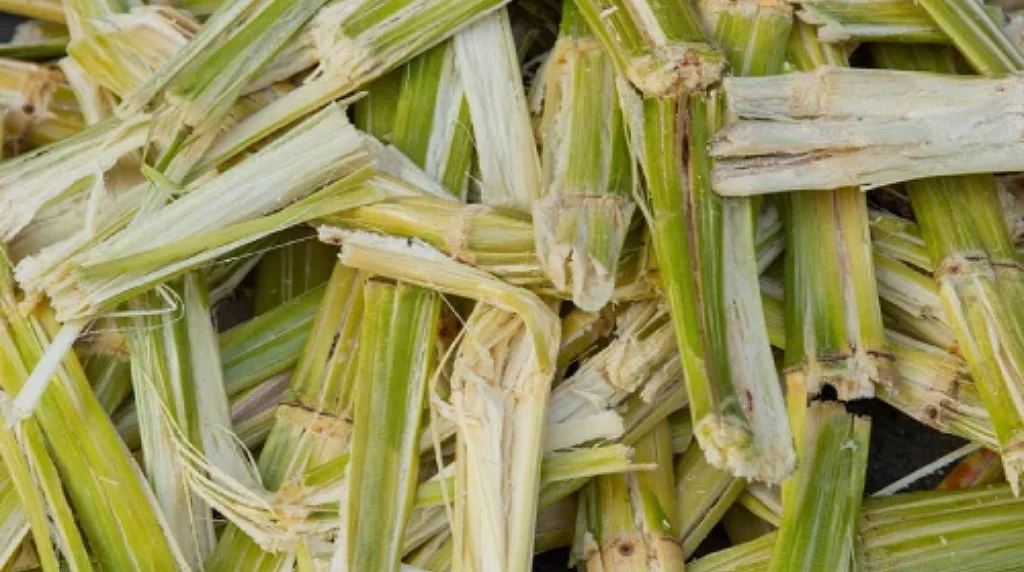
Bagasse

Palm karnel shell

De-Oiled Rice Bran

Jatropha Oil

Corn Cob
Industry Applications

Power Generation

Sugar Mill

Distillery